
A Bespoke Diverter Chute for a KZN Sugar Manufacturer
“The reject brown sugar conveying system has provided our Mill with a practical and reliable solution for managing off-spec brown sugar. The system has improved operational flexibility, reduced manual handling requirements, and helped maintain factory throughput during quality upsets.”

The Project
Every diversion point in a plant is a decision point. Separating packing-grade and reject brown sugar was a critical requirement for a sugar manufacturing operation in KZN. Reject material needed to be diverted away from the main packing plant without disrupting production, while the solution had to integrate into an intricate process built around existing infrastructure.
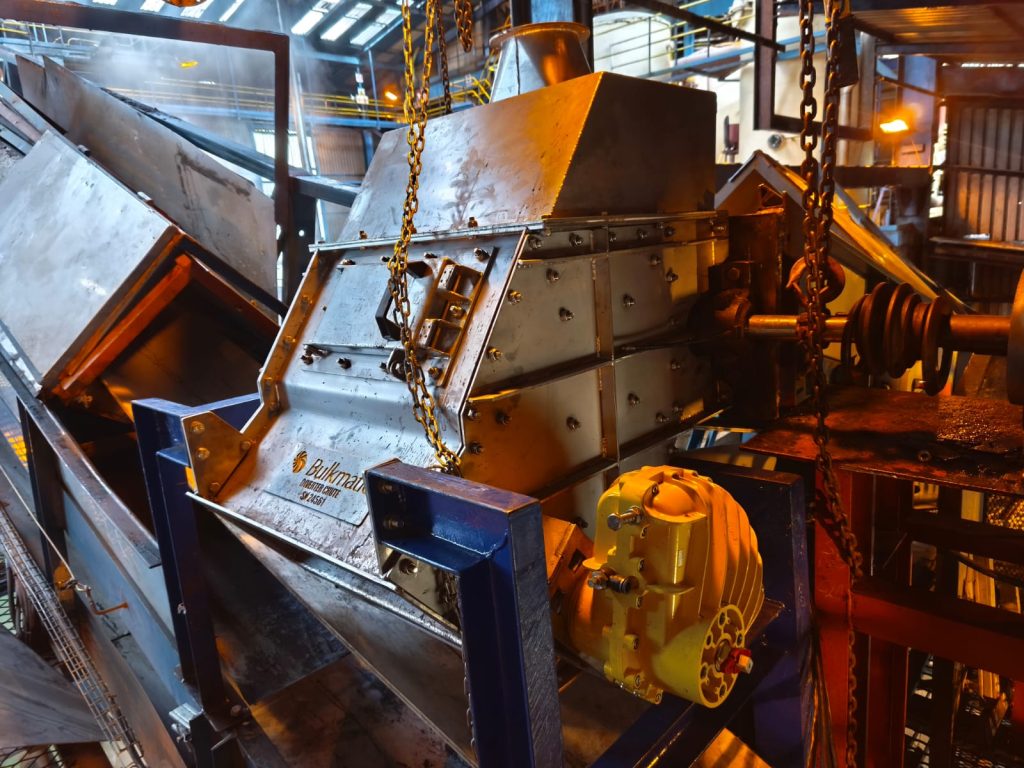
To meet this challenge, Bulkmatic supplied a bespoke 304 stainless steel diverter chute, providing a controlled split between packing-grade and reject sugar. The chute was integrated directly into an existing conveyor discharge, introducing a new routing point into the established process without requiring changes to the surrounding plant layout.
Why It Had to Be Bespoke
Four key constraints shaped the solution and ruled out any off-the-shelf approach.
- The first was the product itself. The chute would be in direct contact with sugar destined for the packing plant, meaning the product-contact surfaces had to meet the required food-grade standards. For this reason, 304 stainless steel was selected instead of coated mild steel, despite the latter being quicker and more cost-effective to manufacture.
- The second constraint was the environment. The installation is located within an ATEX 21/22 zoned area, where fine sugar dust presents a combustible risk. As a result, hazardous-area requirements formed part of the design from the outset rather than being treated as a compliance exercise at the end of the project.
- The third challenge was the existing infrastructure. This was not a greenfield installation. The chute had to be integrated directly into an existing conveyor discharge, with no opportunity to relocate equipment, modify structural elevations, or alter the surrounding layout. The design therefore had to work within the confines of what was already in place.
- Finally, the plant had to remain operational throughout. The purpose of the project was to provide a means of diverting reject material while allowing the packing plant to continue running uninterrupted. Any solution that required production to stop would have defeated the purpose of the system entirely.
Engineering the Retrofit
With the installation site located 727 km from Bulkmatic’s offices, accurate site information was critical. The available space around the installation point was extremely limited, leaving little room for error when designing the new chute and conveyor arrangement.
To overcome this, Bulkmatic trialled a prototype 3D-scanning tool together with an Insta360 camera. A single walkthrough of the area was used to create a detailed 3D point cloud and textured mesh of the existing plant, providing a digital representation of the installation environment.
The resulting digital model was imported into Solid Edge, allowing the design team to check the proposed chute and conveyor against the actual site conditions before procurement and fabrication. This made it possible to verify available space, identify potential clashes with existing equipment, and revisit dimensions from the digital model without requiring another site visit.
For a retrofit where the surrounding infrastructure could not be changed, this gave the design team greater confidence that the completed equipment would fit the first time.
Inside the Chute
The unit consists of a single-inlet, twin-outlet chute manufactured from 304 stainless steel, pneumatically actuated and mounted directly to the conveyor discharge. Sugar enters through the inlet and is directed to one of two outlet legs depending on the position of the diverter blade, allowing material to be routed to the required destination.
The chute body features a bolted construction rather than a fully welded design, with hinged and bolted access covers incorporated into the upper body and side elevations to provide access for inspection and maintenance. This configuration required a balance between food-grade cleanability and maintainability, with smooth, continuous surfaces preferred for the product-contact areas while still providing practical access for inspection and servicing.
The existing conveyor arrangement presented a further design constraint. There was insufficient space for a conventional head chute followed by a separate diverter chute, meaning the diverter could not simply be installed as a downstream component. Bulkmatic instead incorporated the diverter directly into the head chute assembly, effectively combining the two functions into a single piece of equipment. This allowed the required routing function to be accommodated within the existing conveyor arrangement without requiring changes to the surrounding infrastructure.


The Outcome
The completed solution provided the client with a controlled, automated method of separating packing-grade and reject brown sugar. Reject material can be diverted away from the main packing plant without interrupting operations, while the bespoke chute integrates directly with the existing conveyor infrastructure.
The diverter formed part of a wider project scope that included a new mild steel storage silo configured for truck loading, continuous radar level measurement, and emergency high-level safety switches. Together, these systems provide a controlled route for reject material from diversion through to storage and subsequent handling.
The complete scope was designed, fabricated, installed, and commissioned in eight weeks, significantly ahead of the original manufacturing estimate of twelve to fourteen weeks.
Behind the completed installation was a collaborative team effort involving design, documentation, procurement, fabrication, quality assurance, and installation. Delivering a bespoke stainless steel fabrication for a zoned, food-grade environment in just eight weeks required more than a well-designed solution. It required every part of the team to work together and deliver on schedule, demonstrating Bulkmatic’s ability to coordinate and deliver complex, site-specific solutions from concept through to commissioning.
In the Client’s Words
The reject brown sugar system has performed well since commissioning and has achieved the primary objective of allowing off-spec brown sugar to be diverted without impacting refinery operations.
Previously, low-quality brown sugar had to be sent to the refinery or packed into one-ton bags for later reprocessing, both of which negatively impacted throughput and required significant manual intervention.
The new system provides a much more efficient and controlled method of handling reject sugar.
This aligns with the original project objective of protecting refinery throughput and providing a controlled reject route for off-spec brown sugar.
Some of the key benefits observed include:
- Improved factory throughput during brown sugar quality upsets and start-up conditions.
- Reduced reliance on manual handling and reprocessing activities.
- Improved refinery stability by preventing large quantities of off-spec brown sugar from entering the refinery process.
- Operators have responded positively to the system as it provides a practical and user-friendly solution for managing reject sugar.
- The installation has improved operational flexibility and reduced the risk of production interruptions associated with brown sugar quality issues.
At this stage, we have not completed a formal quantification of cost savings, but the operational benefits and improved process stability have been significant.
– Plant Engineering Manager
With over 100 years of combined materials-handling experience, Bulkmatic assists clients with the design, optimisation, and integration of bulk materials-handling systems and equipment. Need technical assistance with conveying, storage, processing, or plant performance challenges? 📩 Contact our team at sales@bulkmatic.co.za or fill in the form below.
